

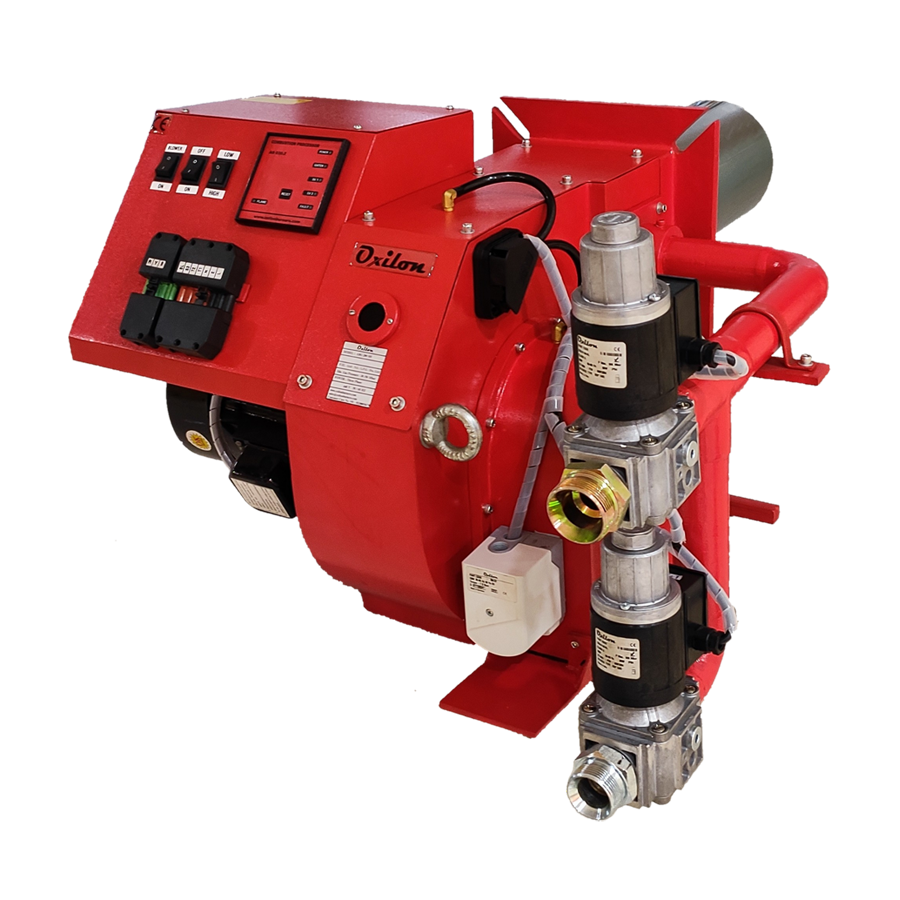
Industrial Burners for Heater Treaters
Efficient Flame Control for Oil & Gas Separation Systems
Heater treaters play a critical role in separating oil, water, and gas in upstream oilfield operations. Our industrial burners are specially engineered to deliver precise, consistent, and safe combustion for these systems — ensuring effective emulsion breaking and process reliability in harsh field environments.
Purpose-Designed for Heater Treater Applications
These burners are built to operate within the firetube of horizontal or vertical heater treaters, providing indirect heat to the production fluids. Combustion efficiency and temperature control are essential to avoid overheating, minimize emissions, and ensure the separation process remains stable.
Key Features
- Optimized Flame Geometry - Engineered to provide complete combustion along the firetube length, avoiding cold spots and flame impingement.
- Rugged Construction - Built to handle harsh field conditions, including sand, wind, moisture, and fluctuating fuel quality.
- Fuel Versatility - Operates on Natural Gas, LPG, Diesel, or wellhead gas, depending on site availability.
- Smart Control Compatibility - Integrates with manual, PID-based, or PLC control panels for temperature regulation and safety shutdowns.
- Field-Serviceable Design - Easy to install, inspect, and maintain in remote locations with limited downtime.
Safety & Compliance
- Flame safeguard system with UV/IR detection
- High-temperature and pressure interlocks
- Automatic shut-off on flame failure or low pilot
- Meets industry-specific codes (CSA, API, CE available)
Technical Specifications (Typical Range)
- Burner Capacity: 50,000 – 1,500,000 kcal/hr.
- Operating Temp Range: Up to 95°C (fluid separation)
- Fuel Types: Gas, LPG, Diesel, Dual-Fuel
Applications
- Crude Oil Heater Treaters
- Free Water Knockouts
- Test Separators
- Remote Oilfield Installations – Off Shore Oil fields
Why Choose Our Burners for Heater Treaters?
- Proven performance in upstream production
- Designed for consistent heat without flame impingement
- Efficient combustion with low maintenance requirements
- Can be retrofitted into existing treaters or supplied with new builds
- Trusted by EPC contractors, OEMs and Many End users like ONGC.


